How Does Steel Wire Deliver Strength and Durability?
2026-09-18
A suspension bridge spanning a deep gorge relies on thousands of steel wires, each thinner than a finger, working together to support millions of kilograms. A tire on a family car contains steel wire so fine and flexible that it can flex millions of times without breaking. A piano string, made from high-carbon steel wire, is tensioned to near its breaking point and must hold that tension for decades. These examples seem unrelated, but they share a common foundation: the remarkable ability of steel wire to deliver strength and durability under conditions that would destroy most other materials. Steel wire is not simply a thin piece of steel; it is a highly engineered product whose properties are the result of precise control over chemistry, microstructure, and manufacturing.
How does steel wire achieve this combination of strength and durability? The answer lies in a multi-stage manufacturing process that transforms a relatively soft steel rod into a wire with exceptional tensile strength, fatigue resistance, and surface integrity. The process involves careful selection of the steel grade, controlled heat treatment, multiple passes through drawing dies, and in some cases, specialized surface coatings. Each stage refines the material's internal structure, reducing defects and aligning the crystal grains in a way that maximizes strength. At Ningbo Dingyan Metal Products Co.Ltd., our factory has been manufacturing steel wire for over two decades, and we have refined every stage of this process to deliver wire that meets the most demanding specifications. This article will provide a comprehensive technical analysis of how steel wire delivers strength and durability, covering the key factors that determine its performance and the applications that depend on it.
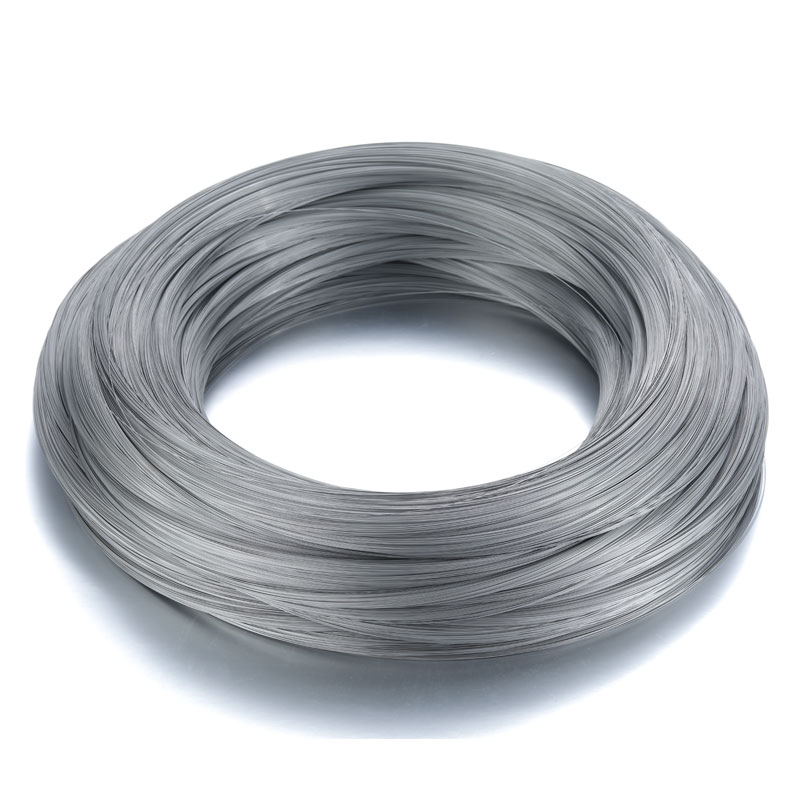
Table of Contents
- 1. The Chemistry of Strength: What Makes Steel Wire Strong?
- 2. The Drawing Process: How Wire Gets Its Strength
- 3. The Heat Treatment Question: When and Why It Matters
- 4. The Surface Story: Coatings That Extend Durability
- 5. The Quality Equation: Testing and Certification for Critical Applications
- 6. Frequently Asked Questions (FAQ)
- 7. Conclusion
1. The Chemistry of Strength: What Makes Steel Wire Strong?
The strength of steel wire begins with its chemical composition. Steel is an alloy of iron and carbon, and the carbon content is the single most important factor determining the wire's strength and hardness. Low-carbon steel, with a carbon content of less than 0.25%, is relatively soft and ductile. It is used for applications such as fencing, nails, and general-purpose wire where formability is more important than strength. Medium-carbon steel, with a carbon content between 0.25% and 0.60%, offers a balance of strength and ductility. It is used for applications such as springs and wire ropes. High-carbon steel, with a carbon content between 0.60% and 1.00%, offers the highest strength and wear resistance. It is used for applications such as tire bead wire, piano wire, and prestressing concrete strand. Our factory at Ningbo Dingyan Metal Products Co.Ltd. produces steel wire across the full range of carbon contents, allowing us to serve a diverse range of applications.
In addition to carbon, other alloying elements are added to achieve specific properties. Manganese is added to improve hardenability and strength. Silicon is added to improve strength and elasticity. Chromium is added to improve corrosion resistance and wear resistance. Vanadium and niobium are added to refine the grain structure and improve toughness. The exact composition of the steel is carefully controlled to ensure that the final wire meets the required specifications. The table below summarizes the typical chemical composition and properties of different steel wire grades.
| Grade | Carbon Content (%) | Typical Tensile Strength (MPa) | Typical Applications |
| Low-Carbon (SAE 1006) | 0.06 - 0.10 | 300 - 500 | Fencing, nails, general-purpose wire |
| Medium-Carbon (SAE 1045) | 0.43 - 0.50 | 600 - 900 | Springs, wire ropes, cables |
| High-Carbon (SAE 1070) | 0.65 - 0.75 | 1,200 - 1,800 | Tire bead, prestressing strand |
| High-Carbon (SAE 1085) | 0.80 - 0.90 | 1,800 - 2,400 | Piano wire, high-strength cables |
| Alloy Steel (SAE 6150) | 0.48 - 0.53 | 900 - 1,500 | High-temperature springs, valve springs |
At our factory, we source our steel wire rod from certified steel mills and verify its chemical composition using spectrometer analysis before it enters production. This rigorous quality control ensures that the final wire consistently meets the required strength and durability specifications. We also work with our customers to select the optimal grade for their application, balancing strength, ductility, and cost.
2. The Drawing Process: How Wire Gets Its Strength
The drawing process is the heart of steel wire manufacturing. It is the process that transforms a relatively soft steel rod into a strong, hard wire. The process begins with a steel rod, typically 5.5mm to 12mm in diameter, which is descaled and cleaned to remove surface oxides. The rod is then coated with a lubricant, such as lime or borax, to reduce friction during drawing. The rod is pulled through a series of dies, each smaller than the last, reducing the diameter and increasing the length of the wire. Each pass through a die reduces the cross-sectional area by approximately 15-25%. The cumulative effect of multiple passes is a dramatic increase in tensile strength. The table below illustrates the relationship between the number of drawing passes and the resulting wire diameter and tensile strength.
| Pass Number | Wire Diameter (mm) | Reduction in Area (%) | Tensile Strength (MPa) |
| Starting Rod | 5.50 | 0 | 450 |
| Pass 1 | 4.80 | 24 | 560 |
| Pass 3 | 3.60 | 44 | 780 |
| Pass 5 | 2.70 | 60 | 1,050 |
| Pass 7 | 2.00 | 72 | 1,350 |
| Pass 9 | 1.50 | 81 | 1,650 |
| Pass 11 | 1.10 | 88 | 1,950 |
The increase in strength during drawing is due to a phenomenon called work hardening, or strain hardening. As the steel is deformed, dislocations in the crystal structure multiply and become entangled, making it more difficult for the material to deform further. This increases the yield strength and tensile strength of the wire. The drawing process also aligns the crystal grains in the direction of the wire, creating a fibrous texture that improves strength and fatigue resistance. At our factory, we use multi-die drawing machines that can draw wire through up to 12 dies in a single continuous operation. The dies are made from tungsten carbide or diamond, and they are carefully maintained to ensure consistent wire diameter and surface quality. We also monitor the drawing speed, lubrication, and temperature to ensure that the wire is not damaged during the process.
3. The Heat Treatment Question: When and Why It Matters
Heat treatment is a critical step in the manufacturing of steel wire for many applications. It is used to relieve the internal stresses created during drawing, to soften the wire for further processing, and to achieve specific mechanical properties. The most common heat treatment processes for steel wire are patenting, annealing, and stress relieving. Patenting is a process used for high-carbon steel wire. It involves heating the wire to a temperature above its critical point (typically 900-950°C) and then cooling it rapidly in a molten lead or salt bath to a temperature of 500-550°C. This produces a fine pearlite microstructure that is ideal for subsequent drawing. Patenting is essential for producing high-strength wire for applications such as tire bead and prestressing strand.
Annealing is a process used to soften the wire and relieve internal stresses. It involves heating the wire to a temperature below its critical point (typically 600-700°C) and holding it there for a period of time before cooling slowly. Annealing is used for low-carbon and medium-carbon wire that will be subjected to further forming operations, such as bending or coiling. Stress relieving is a lower-temperature process (typically 200-400°C) used to relieve the residual stresses from drawing or forming without significantly reducing the strength of the wire. It is used for wire that will be used in fatigue-critical applications, such as springs and wire ropes. The table below summarizes the heat treatment processes and their effects on steel wire properties.
| Process | Temperature Range | Cooling Method | Effect on Properties | Typical Application |
| Patenting | 900 - 950°C | Molten lead or salt bath | Fine pearlite; optimal for drawing | High-carbon tire bead, prestressing strand |
| Annealing | 600 - 700°C | Slow cooling in furnace | Softens wire; relieves stresses | Low-carbon wire for forming |
| Stress Relieving | 200 - 400°C | Air cooling | Relieves residual stresses; maintains strength | Springs, wire ropes, fatigue-critical parts |
At Ningbo Dingyan Metal Products Co.Ltd., our factory operates a fully integrated heat treatment facility with computer-controlled furnaces and lead baths. We monitor the temperature, time, and cooling rate for every batch of wire to ensure that the desired microstructure and properties are achieved. Our metallurgical laboratory verifies the results through microstructural analysis and mechanical testing. This level of control is essential for producing steel wire that delivers consistent strength and durability in the most demanding applications.
4. The Surface Story: Coatings That Extend Durability
The surface of steel wire is vulnerable to corrosion, abrasion, and fatigue. To extend the durability of the wire, a variety of surface treatments and coatings are applied. The choice of coating depends on the application and the environment in which the wire will be used. The most common coatings are galvanizing (zinc coating), phosphate coating, and polymer coating. Galvanizing is the most widely used coating for steel wire. It provides excellent corrosion resistance by forming a barrier between the steel and the environment. The zinc coating also provides sacrificial protection; if the coating is scratched, the zinc will corrode preferentially, protecting the steel underneath. Galvanized wire is used in applications such as fencing, gabions, and marine ropes.
Phosphate coating is a conversion coating that is applied to steel wire to improve its corrosion resistance and its ability to retain lubricants. It is often used as a base for subsequent coatings, such as paint or polymer. Phosphate-coated wire is used in applications such as automotive springs and fasteners. Polymer coating, such as PVC or nylon, provides a thick, durable barrier against corrosion and abrasion. It is used in applications where the wire will be exposed to harsh chemicals or where a colored finish is desired. The table below summarizes the common surface treatments for steel wire and their properties.
| Coating | Thickness (µm) | Corrosion Resistance | Abrasion Resistance | Typical Application |
| Hot-Dip Galvanized | 40 - 80 | Excellent | Good | Fencing, gabions, marine |
| Electro-Galvanized | 5 - 15 | Good | Fair | Indoor applications, fasteners |
| Phosphate | 2 - 5 | Fair | Fair | Springs, fasteners, base for paint |
| PVC Coated | 200 - 500 | Excellent | Excellent | Gardening, animal cages, coastal |
| Nylon Coated | 100 - 300 | Very Good | Excellent | Fishing lines, industrial cables |
At our factory, we offer a full range of surface treatments for our steel wire products. We operate hot-dip galvanizing lines, electro-galvanizing lines, and polymer coating lines. We also provide phosphate coating as a preparatory step for further processing. Our technical team can advise on the best coating for your specific application, considering the environmental conditions, the required lifespan, and the cost. We also test the coating adhesion and corrosion resistance of our products to ensure that they meet the required standards.
5. The Quality Equation: Testing and Certification for Critical Applications
For critical applications such as suspension bridges, elevators, and automotive safety components, the strength and durability of steel wire are not just desirable; they are essential. A failure in these applications can have catastrophic consequences. Therefore, steel wire for critical applications must be subjected to rigorous testing and certification. The testing typically includes tensile testing, torsion testing, bend testing, and fatigue testing. Tensile testing measures the wire's breaking strength and elongation. Torsion testing measures the wire's ductility and its resistance to twisting. Bend testing measures the wire's ability to withstand bending without cracking. Fatigue testing measures the wire's ability to withstand repeated cyclic loading, which is critical for applications such as wire ropes and springs.
In addition to mechanical testing, steel wire for critical applications is often subjected to non-destructive testing (NDT) to detect internal defects such as cracks, inclusions, and porosity. Common NDT methods include eddy current testing, ultrasonic testing, and magnetic particle inspection. The wire may also be tested for its chemical composition and microstructure to ensure that it meets the specified grade and heat treatment. The table below summarizes the key tests for steel wire and their purposes.
| Test | What It Measures | Acceptance Criteria | Typical Application |
| Tensile Test | Breaking strength, yield strength, elongation | Per specification | All critical applications |
| Torsion Test | Ductility, resistance to twisting | Minimum number of twists | Wire ropes, cables |
| Bend Test | Ductility, resistance to bending | No cracking after specified bends | Springs, forming applications |
| Fatigue Test | Resistance to cyclic loading | Minimum number of cycles | Springs, wire ropes, automotive |
| Eddy Current Test | Surface and near-surface defects | No defects above threshold | Critical load-bearing wire |
| Chemical Analysis | Composition of steel | Per grade specification | All applications |
At Ningbo Dingyan Metal Products Co.Ltd., our factory operates a fully equipped testing laboratory with tensile testing machines, torsion testers, fatigue testers, and NDT equipment. We test every batch of wire we produce to ensure that it meets the required specifications. We also provide certification and test reports for our customers, which are often required for regulatory compliance and quality assurance. Our commitment to quality and testing is what makes our steel wire suitable for the most demanding applications.
6. Frequently Asked Questions (FAQ)
Question 1: What is the difference between low-carbon and high-carbon steel wire?
Answer: The primary difference is the carbon content. Low-carbon steel wire contains less than 0.25% carbon and is relatively soft and ductile. It is used for applications such as fencing and nails. High-carbon steel wire contains 0.60% to 1.00% carbon and is much stronger and harder. It is used for applications such as tire bead, piano wire, and prestressing strand. The choice depends on the required strength and ductility for the application.
Question 2: How does the drawing process increase the strength of steel wire?
Answer: The drawing process increases strength through work hardening. As the wire is pulled through progressively smaller dies, the steel is plastically deformed. This deformation causes dislocations in the crystal structure to multiply and become entangled, making it more difficult for the material to deform further. The result is an increase in yield strength and tensile strength. The drawing process also aligns the crystal grains in the direction of the wire, improving strength and fatigue resistance.
Question 3: What is patenting, and why is it important for high-carbon steel wire?
Answer: Patenting is a heat treatment process used for high-carbon steel wire. It involves heating the wire to 900-950°C and then cooling it rapidly in a molten lead or salt bath to 500-550°C. This produces a fine pearlite microstructure that is ideal for subsequent drawing. Patenting is important because it provides the optimal combination of strength and ductility for the wire to withstand the severe deformation of the drawing process without breaking.
Question 4: How does galvanizing protect steel wire from corrosion?
Answer: Galvanizing protects steel wire from corrosion in two ways. First, the zinc coating forms a physical barrier that prevents moisture and oxygen from reaching the steel. Second, the zinc provides sacrificial protection. If the coating is scratched or damaged, the zinc will corrode preferentially, protecting the steel underneath. This is because zinc is more electrochemically active than steel. Galvanized wire is widely used in outdoor and marine applications.
Question 5: What tests are performed to ensure the quality of steel wire?
Answer: The tests performed depend on the application, but common tests include tensile testing (to measure breaking strength and elongation), torsion testing (to measure ductility), bend testing (to measure resistance to bending), and fatigue testing (to measure resistance to cyclic loading). Non-destructive tests such as eddy current testing may also be performed to detect internal defects. At Ningbo Dingyan Metal Products Co.Ltd., we test every batch of wire to ensure it meets the required specifications.
7. Conclusion
Steel wire is a remarkable material that delivers strength and durability through a combination of careful chemistry, precise manufacturing, and rigorous quality control. The carbon content determines the wire's strength and hardness. The drawing process increases strength through work hardening and aligns the crystal grains. Heat treatment refines the microstructure and relieves internal stresses. Surface coatings protect the wire from corrosion and abrasion. And testing ensures that the wire meets the requirements of the most demanding applications. At Ningbo Dingyan Metal Products Co.Ltd., our factory has mastered every stage of this process, and we are proud to supply steel wire that our customers trust for their most critical applications.
Whether you are designing a suspension bridge, manufacturing automotive components, or producing industrial wire ropes, the strength and durability of your steel wire are essential to your success. We invite you to contact our technical team to discuss your specific requirements. We can help you select the right grade, coating, and heat treatment for your application. Our commitment to quality and customer satisfaction has made us a trusted partner for steel wire customers around the world.
Contact Ningbo Dingyan Metal Products Co.Ltd. today to discuss your steel wire requirements and discover how our products can deliver the strength and durability your applications demand.